 135-6073-0094
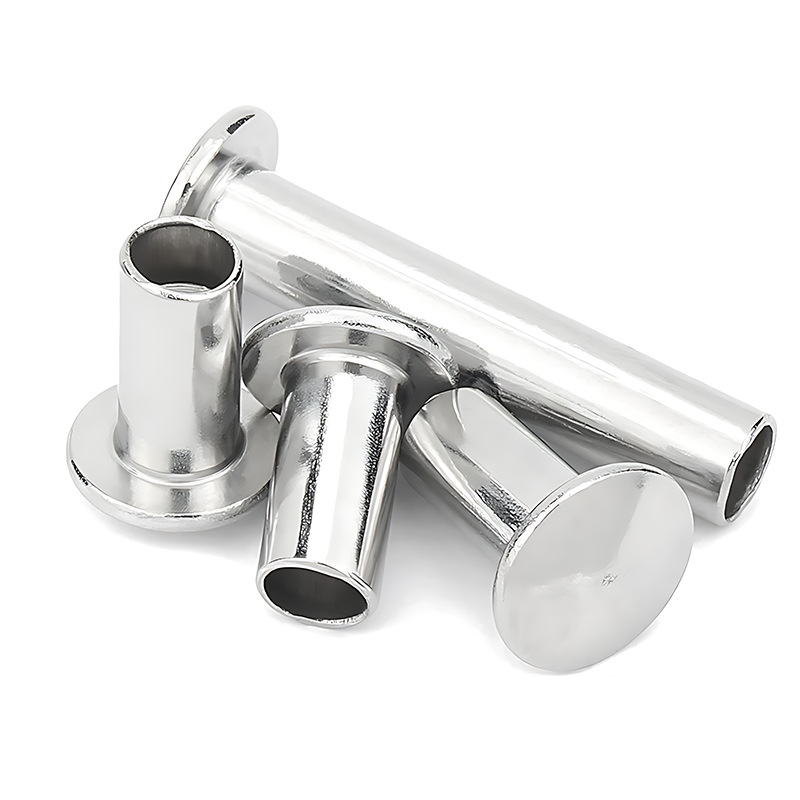
In the fastener manufacturing supply chain, heat treatment is a pivotal process that bridges preceding and subsequent steps. It directly determines critical mechanical properties such as hardness, strength, and toughness, and ultimately dictates application safety in sectors like automotive, aerospace, and construction machinery. What appears to be a routine heating and cooling process actually conceals numerous technical intricacies. The slightest oversight can lead to issues like insufficient hardness, deformation, cracking, or uneven performance, potentially triggering major safety accidents. Practice has proven that mastering four core points is essential to circumventing quality risks at the source and laying a solid foundation for fastener quality.
Temperature is the "soul" of heat treatment. Different materials and specifications of fasteners have strict temperature thresholds. Precise control is the foundation for ensuring adequate microstructural transformation and meeting performance standards. For example, for common Grade 45 steel bolts, the quenching temperature must be controlled between 820-840°C. A temperature that is too low results in incomplete austenitization, failing to form a uniform martensitic structure after cooling, leading to inadequate hardness and strength. Conversely, excessively high temperatures cause coarse austenite grains, reducing toughness, increasing brittleness, and making the fastener prone to fracture during use. In practice, three aspects require attention:
- High-Precision Equipment: Use accurate heating equipment such as medium-frequency induction furnaces or box-type resistance furnaces, equipped with professional pyrometers to monitor furnace temperature in real-time and avoid excessive temperature gradients.
- Customized Heating Curves: Develop personalized heating curves based on material composition, defining heating rates and holding times. For instance, alloy steel fasteners require slower heating rates to prevent deformation caused by thermal stress.
- Optimal Loading Density: Avoid overly dense stacking of fasteners to ensure heating uniformity. Especially in mass production, the furnace loading capacity must be reasonably controlled to ensure every fastener is fully heated.
The cooling phase directly determines the final microstructure and is a key step influencing ultimate performance. Both excessively fast and slow cooling speeds can lead to defects. Different materials require corresponding cooling media and methods:
- Carbon Steel: Typically uses water quenching for its fast cooling speed, rapidly obtaining a martensitic structure to enhance hardness.
- Alloy Steel: Often employs oil quenching. The slower cooling rate reduces quenching stress and lowers the risk of deformation and cracking.
- High-Toughness Requirements: Some fasteners require air cooling or slow cooling to avoid excessively high hardness.
Pre-treatment before heat treatment is often overlooked but directly impacts the outcome. Common steps include surface cleaning, fixturing, and stress relief. Surface cleaning must remove oil, rust, and oxide scale; residues can form localized oxidation or decarburization layers during heating, reducing surface hardness and wear resistance. Fixturing requires selecting appropriate jigs to avoid additional stress from overtightening or positional shifts from loose clamping. For stamped or forged fasteners, stress-relief annealing is necessary to eliminate internal stresses generated during processing, preventing deformation from stress superposition during heat treatment. Additionally, visual inspections should screen out billets with cracks or scratches to prevent defective raw materials from entering the heat treatment stage and causing cost waste.
Post-heat treatment inspection is the final line of defense. A comprehensive testing system must cover hardness, metallographic structure, dimensional accuracy, and appearance.
- Hardness Testing: The fundamental item. Use Brinell, Rockwell, or Vickers hardness testers according to product standards. Sampling must be uniform, focusing on critical stress areas like threads and heads.
- Metallographic Analysis: Use professional equipment to observe the microscopic structure, confirming the formation of uniform target structures like martensite or pearlite, and eliminating defects such as overheated structures or Widmanstätten structures.
- Dimensional Accuracy: Re-check dimensions like outer diameter, length, and thread precision using calipers, micrometers, or projectors to correct or reject deformed products.
- Appearance Inspection: Screen for oxide scale, cracks, or deformation to ensure compliance with assembly requirements. Simultaneously, maintain detailed inspection records to establish a quality traceability system for future troubleshooting and process optimization.